3D Puff Embroidery Cap Issues and How to Fix Them Properly (2026)
Published September 10, 2026 | By USA Digitizing Pro Team
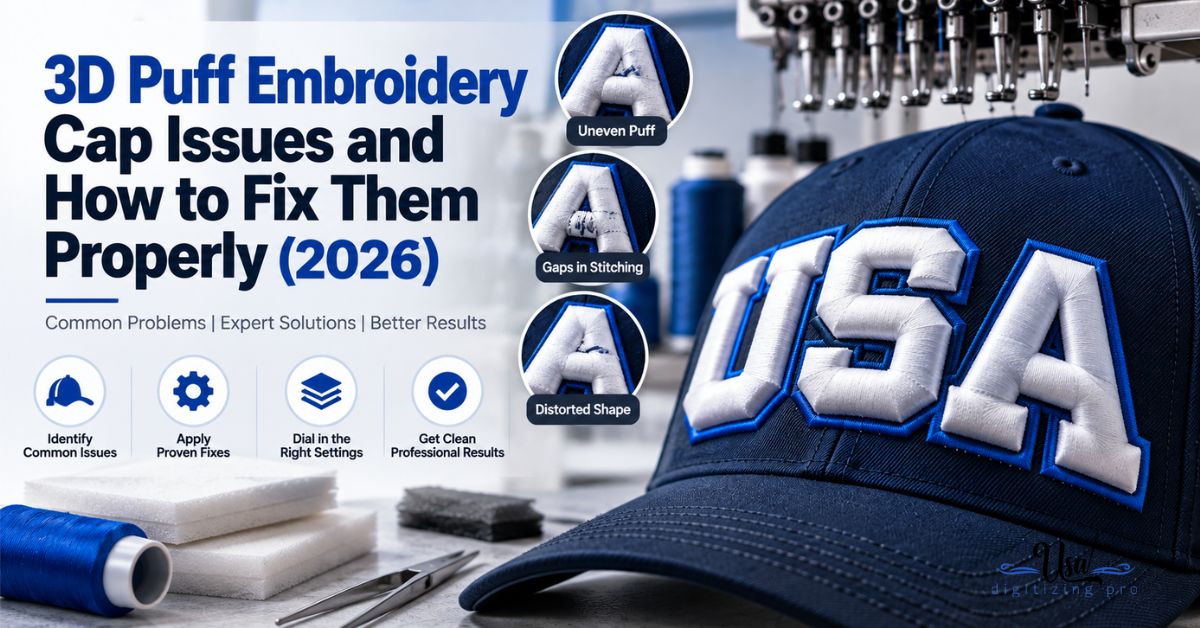
Puff on caps fails in ways flat puff never does, and the arguments about why usually split along predictable lines. Digitizers blame the file, operators blame the machine, and both are sometimes right. The useful move is sorting which category your specific symptom belongs to before changing anything, because a rebuild will not stop a needle breaking on a centre seam and a new needle will not stop foam showing through thin coverage.
Quick Answer at a Glance
| Symptom | Most Likely Cause | Where the Fix Lives |
|---|---|---|
| Foam visible through the thread | Capping density too light to enclose the edge | File |
| Letters flat or collapsed | Column narrower than the foam can support | File |
| Ragged foam left after tear-away | Column width mismatched to foam thickness | File |
| Foam springing back at corners | Stitch length too long through the turn | File |
| Needles snapping | Cap flagging at the centre seam, wrong needle | Machine and floor |
| Thread breaking repeatedly | Speed too high, friction on tight buckram | Machine and floor |
| Crooked or drifting logo | Cap frame movement during the run | Machine and floor |
Why Caps Are Harder Than Flat Puff
Three structural facts about a cap make puff behave differently there than on a jacket back. Every issue further down traces back to one of them.
The Curved Panel
A cap front curves away from the needle in two directions at once, so the fabric under one end of a satin column sits at a different angle to the needle than the other end. Foam compounds this by adding height to a surface that was already not flat. This is why puff settings that work perfectly on a flat garment need adjustment before they run on a cap. the caps versus jackets puff comparison covers what changes between the two surfaces.
The Centre Seam
Most structured caps carry a seam straight up the middle of the front panel, and that seam is thicker and stiffer than the fabric either side of it. A design crossing it asks the needle to punch through a raised ridge while the cap is already curved and under tension in the frame. Ragged edges and deflection both concentrate at that crossing point.
Buckram and Structure
Structured caps have buckram behind the front panel, which is what keeps them upright. It also means the needle is passing through a stiff extra layer on every stitch, generating friction and resistance that a soft unstructured cap never produces. Tight buckram plus high machine speed is a specific and avoidable combination. the structured versus unstructured cap guide covers how the two constructions differ.
Foam and Coverage Issues
These are the faults most people mean when they report a puff problem, and all three sit squarely in the digitizing file rather than on the production floor.
Foam Showing Through the Stitching
Micro-gaps in the satin let the foam colour show between threads. The cause is capping density set too light to fully enclose a raised edge, since puff satin has to close around foam rather than lie flat on fabric. Raising density is the real fix. As an interim measure, matching the foam colour to the thread colour disguises small exposures well enough to save a batch already in production.
Letters Collapsing or Losing Height
A letter that stitches out flat rather than raised usually means the column was too narrow for the foam beneath it, so the capping stitches compressed the foam instead of enclosing it. Heavy satin fills and tightly packed stitching over too narrow a span push the foam down. The other frequent cause is a zigzag underlay left in the file, which flattens the foam before the top stitches ever reach it.
Columns Too Narrow to Hold Foam
US sources put the minimum puff column width anywhere from a 3mm absolute floor up to a 6mm recommendation for cap work specifically, and the safer figure on caps is the higher one. Anything narrower cannot physically hold foam in position under capping stitches. Elements below that width should be converted to flat embroidery within the same design rather than forced into puff. the puff foam and width settings guide covers pairing column width to foam thickness.
Edge and Corner Issues
Corners and turns are the highest risk areas in any puff design, and on a curved cap panel they concentrate every problem the flat version would have shown mildly.
Ragged Tear-Away at the Edges
When excess foam refuses to tear cleanly and leaves fluff along the edges, the satin did not perforate it properly. That comes back to column width being mismatched to the foam thickness, or capping stitches running too long to punch through. The centre seam makes this noticeably worse, since the needle is crossing an uneven raised area on a curved surface at that point.
Foam Springing Back at Corners
Foam compresses under stitches and wants to spring back where coverage thins out, and corners are exactly where coverage thins. Reducing stitch length through the turn, to around 2.0mm or shorter at the corner specifically, packs more stitches into the tightest part and holds the foam down. This is a targeted adjustment at the corner rather than a change across the whole element.
Why Rounding Corners Helps
Sharp inside and outside corners give foam a point to escape from and give the satin a turn too tight to cover cleanly. Softening those corners slightly during digitizing reduces both foam exposure and frayed edges, and on most logos the visual difference is negligible while the production difference is substantial. the corner capping methods guide covers corner treatment in flat work, and the same principles tighten up under foam.
Machine-Side Issues
These three have nothing to do with the file, which is why rebuilding a design never resolves them. They are the half of cap puff troubleshooting that digitizing-focused articles tend to skip.
Needle Breaks and Cap Flagging
Flagging is the cap bouncing or lifting against the frame as the needle works, and it is worst at the centre of the front panel where the seam sits and where the frame supports the cap least. That extra movement deflects the needle sideways until it snaps. Better frame tension and correct cap positioning reduce it, and needle choice matters as covered below.
Thread Breaks and Thread Melt
Repeated thread breaks on cap puff come from several places at once: dense stitch areas, foam resistance, the seam crossing, and tension. There is also a specific failure where high machine speed combined with tight buckram generates enough friction to melt the thread rather than snap it cleanly. Slowing the machine down on puff runs is a real fix, not a workaround.
Needle Selection
Needle choice on structured caps with puff is worth getting right, and an 80/12 sharp is a commonly recommended option for reducing deflection through buckram and foam. A needle that is too fine deflects, and a dull needle drags and increases friction on an already high friction job. Fresh needles matter more on puff than on standard cap work.
Which Fixes Belong in the File
Sorting this correctly saves rerunning the wrong solution, which is the most expensive part of most puff troubleshooting.
What Only a Rebuild Can Change
Capping density, column widths, corner stitch length, presence of a zigzag underlay, stitch sequencing, and which elements are puffed rather than flat are all locked in the file. No frame tension, needle change, or speed adjustment touches any of them. If the symptom is foam showing, collapsed letters, or ragged tear-away, stop adjusting the machine.
What the Operator Controls
Frame tension, cap positioning, machine speed, needle type and freshness, foam colour choice, and the trim and cleanup after the run all sit on the floor. If the symptom is needle breaks, thread melt, or a logo drifting during the run, the file is probably fine. the cap embroidery troubleshooting guide covers the same file versus floor split for standard cap work.
Preventing It on the Next Run
Most cap puff problems are visible on a single test cap, which makes the sample step the cheapest quality control available on this kind of work.
Pre-Production Checklist
- Confirm every puffed element sits comfortably above the minimum column width for cap work.
- Check the file for any zigzag underlay in puff areas and remove it.
- Reduce stitch length through corners to hold foam at the turns.
- Soften sharp inside and outside corners before building the file.
- Fit a fresh sharp needle suited to structured caps and puff.
- Drop machine speed for the puff run, then test on an actual cap and inspect the tear-away.
A Real Order, Broken Down
A Texas cap decorator ran a puffed wordmark and reported three problems at once: foam visible along the letter edges, two snapped needles, and ragged foam that would not tear away. Sorting them apart took one test cap. The foam showing and the ragged tear-away were file faults, thin capping density and columns too narrow for the 3mm foam in use, and both needed a rebuild. The needle breaks were not: they were happening where the design crossed the centre seam, with the cap flagging in the frame at exactly that point. Retensioning the frame and moving to a sharper needle stopped those, while the rebuild fixed the other two. Rerunning the file alone would have solved two problems out of three and left the operator convinced the digitizer had missed something. the sink prevention guide for curved caps covers the related loss-of-height problem on curved panels.
Who Builds These Files
USA Digitizing Pro builds cap puff files from its Texas studio, setting capping density for full foam encapsulation, matching column widths to the foam in use, and handling corners so the tear-away comes clean. Pricing starts at $15 for designs under 5 inches, with a 2 to 4 hour turnaround and a money-back quality guarantee. Service details are on the 3D puff digitizing page and the cap digitizing page.
Frequently Asked Questions
Capping density is too light to fully enclose the raised foam edge, leaving micro-gaps between stitches. Raising density is the fix, and matching foam colour to thread colour disguises small exposures on work already in production.
Either the column was too narrow for the foam, so the capping stitches compressed it rather than enclosing it, or a zigzag underlay in the file flattened the foam before the top stitches ran.
US sources give a range, from a 3mm absolute floor up to a 6mm recommendation for cap work specifically. The higher figure is the safer working minimum on caps, and narrower elements should be digitized flat.
The satin never perforated the foam properly, usually because column width does not suit the foam thickness or capping stitches are too long. The centre seam makes it worse where the design crosses it.
Cap flagging, meaning the cap moving against the frame, deflects the needle until it snaps. It is worst at the centre of the front panel where the seam sits. Better frame tension and a needle suited to structured caps both help.
An 80/12 sharp is commonly recommended for reducing deflection through buckram and foam. Freshness matters as much as size, since a dull needle drags and adds friction to an already high friction job.
Dense areas, foam resistance, and the seam crossing all contribute. Thread melt specifically comes from high machine speed combined with tight buckram generating friction, so slowing the machine is a genuine fix.
Yes, softening sharp inside and outside corners reduces foam exposure and frayed edges at turns, and on most logos the visual change is negligible compared with the production improvement.
Foam showing, collapsed letters, ragged tear-away, and corner problems are file faults. Needle breaks, thread melt, and a logo drifting during the run are machine and floor issues.
Diagnose Before You Rerun
3D puff embroidery cap issues fall into two piles, and mixing them up is what turns a one day fix into a three week argument. Foam showing, flat letters, ragged edges, and corner problems live in the file and need a rebuild. Needle breaks, thread melt, and drift live on the production floor and need frame tension, needle choice, and speed adjustments. Sort the symptom first, fix the right side, and the next run comes off clean.
Follow Us

RELATED BLOGS
Hat Machine Embroidery: What the Machine Decides About.
Published October 2, 2026 | By USA Digitizing Pro Team Hat machine embroidery looks like a software problem and it is mostly.
Logo Digitizing Stitch Count Estimator Guide: Rough Numbers.
Stitch count sounds like a technical detail buyers shouldn't have to think about, until a quote comes back higher than expected and.
1 COMMENT
[…] of the panel while the edges stand up fine. That uneven pattern across the design is the tell. the puff cap issue diagnosis guide covers the other two faults in […]